Description
API 8C Weldless Элеватор Link – Overview
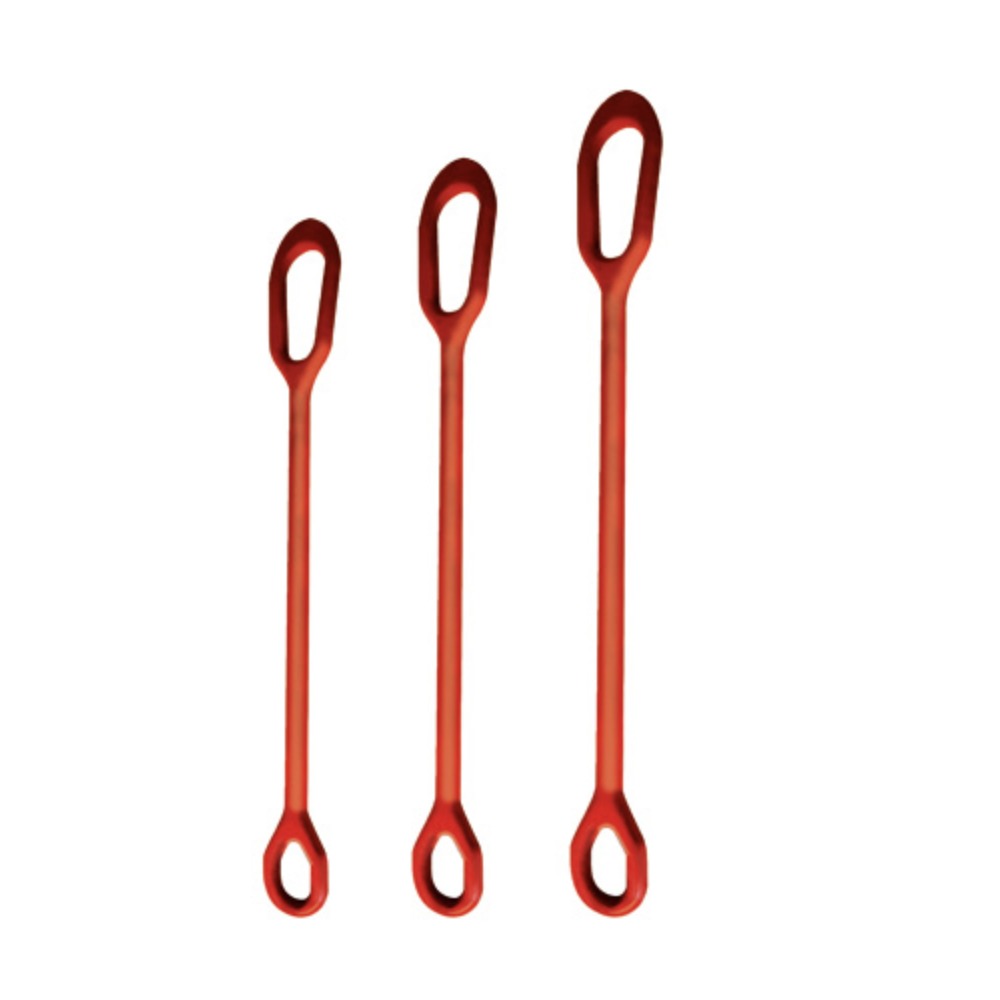
The CAMTOP Weldless Элеватор Link is a single-piece, forged alloy-steel connector designed to join the traveling block hook to the drill pipe / casing / tubing elevator on drilling rigs, completion rigs, and workover rigs. Manufactured per API Spec 8C (PSL 1 & PSL 2) with no welds in any load-bearing path, the weldless link delivers superior fatigue life, predictable ductility, and the redundancy needed for deep and ultra-deep well operations where conventional welded links cannot pass the API 8C dynamic-load qualification.
Available in rated capacities from 50 to 750 short tons and seven standard lengths from 1100 mm to 6700 mm, the CAMTOP weldless elevator link family is interchangeable with industry-standard links (RUTONG DH series, Oil Country, Myers, BJ, Varco) and is supplied with full traceability, load-test certificates, and color-coded identification for fast field recognition.
Product Image
Key Features
- Single-Piece Monoblock Construction — drop-forged from a single alloy-steel billet; no welds, no bolted joints, no failure points along the load path.
- API Spec 8C PSL 1 / PSL 2 Compliant — manufactured and tested in accordance with API Spec 8C drilling and production hoisting equipment.
- Capacity Range 50-750 Short Ton — DH50 / DH75 / DH150 / DH250 / DH350 / DH500 / DH750 ratings cover virtually every drilling and workover elevator on the market.
- Standard Lengths 1100 mm to 6700 mm — DH150 supplied in 12 incremental lengths (1800/2100/2400/2700/3000/3300/3600/3900/4200/4500/5400/6700 mm) for 100-, 150-, 250-, 350-ton elevators.
- High-Strength Alloy Стальной — quench-and-tempered alloy steel (AISI 4140 / 4340 / EN 10083 equivalent) for high tensile strength and impact toughness at sub-zero temperatures.
- Machined Eye Подшипник Surfaces — both eye ends are CNC-machined for precise inner-diameter tolerance, smooth shackle articulation, and reduced wear on mating pins.
- Shot-Blasted & Painted Finish — red oxide primer + safety-red polyurethane topcoat (RAL 3000 standard); color-coded per load rating for instant field identification.
- Color-Coded by Tonnage — industry-standard color recognition (DH50 red / DH75 black / DH150 blue / DH250 green / DH350 yellow / DH500 silver / DH750 orange).
- 100% Magnetic-Particle Inspected — every link is MT/PT-tested across the full load path; critical areas receive supplementary UT examination.
- Proof-Load Tested — each link is loaded to 1.25x WLL and a sample from each lot is loaded to destruction; certificates and MTC 3.1 supplied.
- Drop-Кованый & Machined Eyes — upset-forged eye ends produce continuous grain flow around the bearing surface, eliminating fatigue initiation from machining.
- Becket & Clevis Compatible — standard eye dimensions suit Becket / McKissick / Crosby / S-2798B shackles, crown-o-matic swivels, and most traveling-block safety hooks.
- NACE MR0175 Sour Service Optional — HIC-resistant alloy and SS316 bearing pins available for sour-service (H₂S) environments.
- Modular Field Serviceability — eyes accept standard replacement shackle pins, allowing swap-out without scrapping the entire link.
Technical Specifications
| Parameter | Specification |
|---|---|
| Design Standard | API Spec 8C (PSL 1 & PSL 2) |
| Manufacturing Process | Single-piece closed-die drop forging, Q&T |
| Material | Alloy steel (AISI 4140 / 4340 / EN 10083 42CrMo4) |
| Rated Load Range | 50 / 75 / 150 / 250 / 350 / 500 / 750 short ton |
| Length Options | 1100 mm to 6700 mm (model-dependent) |
| Eye Inner Diameter | Ø 60 mm to Ø 180 mm (model-dependent) |
| Bar Stock Diameter | Ø 32 mm to Ø 110 mm |
| Ultimate Tensile Strength | 930 – 1080 MPa (135 – 157 ksi) |
| Yield Strength | 690 – 850 MPa (100 – 123 ksi) |
| Elongation (min) | ≥ 12% (2-inch gauge) |
| Reduction of Area (min) | ≥ 35% |
| Charpy Impact @ -20 °C | ≥ 27 J (20 ft-lbf) |
| Surface Hardness | 285 – 363 HBW |
| Proof Load Test | 1.25 x WLL held 30 seconds |
| Production Sample Load Test | 1 lot per 25 links loaded to 2.0 x WLL |
| NDT Method | Magnetic Particle (MT) per ASTM E709; UT on request |
| Surface Finish | Shot-blast SA 2.5 + red PU paint (RAL 3000) |
| Service Temperature | -46 °C to +121 °C (-50 °F to +250 °F) |
| Service Environment | Standard / Sour Service (NACE MR0175 optional) |
| Marking | Embossed: manufacturer, model, WLL, serial, heat # |
| Traceability | MTC EN 10204-3.1 per link; full PMI on request |
| Recommended Shackle | Crosby G-2130 / S-2798B (matched by WLL) |
Available Models – Weldless (DH) & Perfection (SH) Series
DH series = weldless links for deep / ultra-deep well drilling (no welds along the load path).
SH series = perfection (welded) links for shallow well drilling and workover (cost-optimized design).
| Series | Model | Rated Load (Short Ton) |
Standard Lengths (mm) |
Compatible Элеватор | Recommended Service |
|---|---|---|---|---|---|
| DH Weldless |
DH50 | 50 t | 1100 | 100 t elevator | Shallow / medium-depth drilling |
| DH75 | 75 t | 1500 | 150 t elevator | Medium-depth drilling, workover | |
| DH150 | 150 t | 1800 / 2100 / 2400 / 2700 / 3000 / 3300 / 3600 / 3900 / 4200 / 4500 / 5400 / 6700 | 150 / 250 t elevator | Deep & ultra-deep drilling | |
| DH250 | 250 t | Per spec | 250 t elevator | Deep drilling, completion | |
| DH350 | 350 t | Per spec | 350 t elevator | Deep drilling, HPHT | |
| DH500 | 500 t | Per spec | 500 t elevator | Ultra-deep drilling | |
| DH750 | 750 t | Per spec | 750 t elevator | Ultra-deep, offshore drilling | |
| SH Perfection |
SH75 | 75 t | 1500 | 150 t elevator | Shallow drilling, workover |
| SH100 | 100 t | 1500 | 100-150 t elevator | Shallow drilling | |
| SH150 | 150 t | 1700 | 150 t elevator | Shallow drilling, completion |
Working Principle & Operating Environment
- Hook-to-Элеватор Coupling — top eye attaches to the traveling-block hook (or crown-o-matic hook); bottom eye connects to the elevator body via a captive shackle pin (Becket / Crosby G-2130 style).
- Single-Piece Load Path — hook load → top eye → forged shank (continuous grain flow) → bottom eye → shackle pin → elevator body. No welds, no bolted transitions — the entire load travels through a single forged metal path.
- Triaxial Load Management — designed to withstand combined tension (hook load), bending (rotary-table rotation), and cyclic fatigue (trips in/out of hole) without developing stress concentrations.
- Shock Absorption at the Eye — the generous eye inner-diameter clearance allows the shackle pin to articulate ±5° under side-load, isolating the link shank from bending moments induced during pickup / setdown.
- Fatigue Resistance — Q&T alloy steel with surface finish > 3.2 Ra µm and 100 % MT inspection ensures the link passes the API 8C 20,000-cycle endurance test at 1.33 x WLL.
- API 8C PSL 2 Dynamic Rating — PSL 2 weldless links additionally qualify for dynamic loading envelopes (1.5 x WLL transient) found in rough-neck make-up / breakout operations.
Manufacturing & Quality Control
- Forging — closed-die upset forging of vacuum-degassed alloy-steel billet; eye ends are formed with continuous grain flow around the bearing surface.
- Heat Treatment — normalize → austenitize → oil quench → temper, calibrated to ASTM A370 mechanical property targets.
- Machining — CNC turning of eye inner diameters, bearing surfaces, and pin bores; tolerances held to ±0.05 mm on critical fit surfaces.
- NDT 100 % — wet fluorescent magnetic-particle inspection (ASTM E709) over the entire eye surface and shank; UT scan for sub-surface defects in eye transition zones.
- Mechanical Testing — every heat lot: tensile (yield / UTS / elongation / RA), Charpy impact at -20 °C, Brinell hardness.